

PRODUCTDETAILS
-
Catalytic combustion equipment
-
Single Baghouse Dust Collector
-
Baghouse Dust Collector
-
Industrial Dust Collector
-
Filter Bag
-
Filter Bag Cage
-
Pulse Jet Valve
-
Screw Conveyor
-
Rotary Airlock Valve
-
Ventilation Butterfly Valve
-
Knife Gate Valve
-
Grinding Downdraft Table
-
Activated Carbon Adsorption Box
-
UV photocatalytic waste gas treatment
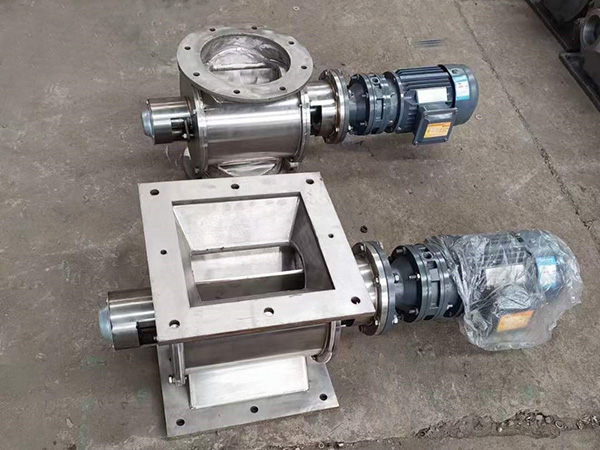
Stainless Steel Rotary Airlock Valve
The Stainless Steel Rotary Airlock Valve is a high-performance bulk material handling component,distinguished by its all-stainless-steel construction that delivers exceptional corrosion resistance,hygiene,and durability.As a key part of pneumatic conveying systems,gravity feeding lines,and bulk storage setups,it fulfills two critical functions:enabling the continuous,controlled transfer of dry bulk materials and maintaining an airtight seal between different pressure zones,thus ensuring system efficiency and stability.
Crafted from high-quality stainless steel materials—commonly 304,316,or 316L stainless steel—the valve is specifically designed to address the challenges of harsh or hygienic industrial environments.304 stainless steel offers excellent resistance to general corrosion and oxidation,making it suitable for most common applications,while 316 and 316L variants provide enhanced resistance to acidic,alkaline,and saline environments,as well as better performance in high-humidity conditions.The entire structure,including the housing,rotor,vanes,and flanges,is made of stainless steel,eliminating the risk of material contamination and ensuring compliance with strict hygiene standards.
Its operating principle is efficient and reliable:driven by a motor and gearbox,the rotor with evenly spaced vanes rotates within the stainless steel housing.Bulk materials—such as powders,granules,or pellets—enter the valve through the inlet,fill the pockets between the vanes,and are carried to the outlet as the rotor turns.The precision-machined tight tolerance between the rotor and housing ensures an effective airtight seal,preventing backflow of air or gas and maintaining the pressure integrity of the conveying system,even under varying pressure differentials.
This valve is widely used in industries that demand high hygiene standards,corrosion resistance,or clean operation,including food and beverage processing,pharmaceutical manufacturing,chemical processing,water treatment,semiconductor manufacturing,and cosmetic production.It efficiently handles materials such as food powders,pharmaceutical ingredients,chemical reagents,activated carbon,and sterile granules,without causing contamination or material degradation.
Key advantages of the Stainless Steel Rotary Airlock Valve include superior corrosion resistance,excellent hygiene performance(easy to clean and sanitize),rugged construction for long service life,and compatibility with sterile or corrosive environments.Optional configurations,such as food-grade seals,polished inner surfaces,variable speed drives,and replaceable wear-resistant rotor tips,further customize the valve to meet specific application needs.With its reliable performance and high adaptability,it has become an indispensable component in high-standard bulk material handling systems.
 BLOGS
-
Stainless Steel Filter Cage vs Galvanized: Which to Choose
2026-10-23 09:48:36
-
How to Choose a Custom Filter Cage Manufacturer: A Buyer's Guide
2026-10-22 09:45:40
-
Filter Bag Micron Rating Explained for Industrial Filtration
2026-10-20 04:28:54
-
Screw Conveyor Capacity Calculation: Complete Engineering Guide
2026-10-19 04:13:28
-
Industrial Screw Conveyor System: Complete Working Principle and Applications Guide
2026-10-18 02:39:26
CONTACT US